Commercial building entrances put column covers and canopy soffits in the same sight line. A visitor approaching the door reads the wrapped column, the underside of the canopy, and the transition between them as one surface field. When those pieces arrive from separate product decisions—one sheet for the column, another for the soffit, with different fold returns, coating lots, or cassette depths—the entrance looks patched even if each part meets its own drawing note. The conflict is geometric and visual at the same time: columns need tight wrap tolerances around a structural column, while canopy soffits need flat, continuous undersides that hide framing, lighting, and drainage details.
Aluminum Composite Panel is widely used for both roles because fabricators can route the reverse face and fold sheets into cassettes with returns that engage a subframe. That capability is useful only when the entrance is planned as one cladding skin. Column faces often take more direct weather and touch traffic near doors; soffit undersides sit in reflected light and collect soiling differently. Those conditions still share the same coated face language if the project wants a coherent lobby approach. Treating the entrance as two unrelated packages is how color drift, mismatched returns, and irregular joint rhythm appear after install.
Rucobond is a manufacturer and supplier of architectural panels, including Aluminum Composite Panels for building exterior and related cladding applications such as column covers and canopy soffit work. Fabricators remain responsible for routing, folding, and cassette assembly; installers remain responsible for fixing systems and site installation. Entrance programs may also use solid Aluminum Veneer where fold depth or stiffness needs exceed what a composite cassette can handle cleanly. The sections that follow stay on that entrance path: geometry, fold design, routing practice, material limits, coating roles, nesting and packing, joint continuity, and the drawing fields that make a purchase enquiry usable.
A column cover cassette and a canopy soffit tray solve different geometric jobs even when they share the same ACP product. Column wraps typically form a closed or near-closed polygonal shell around a structural column. Returns must clear the subframe, leave room for fasteners or clips, and keep the visible joint consistent around the perimeter. Radius or chamfered corners on the column elevation require either carefully planned fold miters or separate corner pieces. Tall columns also stack vertically, so horizontal joints must align with floor or reveal lines already fixed in the architectural drawings.
Canopy soffit trays face downward. The visible face is the underside; returns usually turn up into a secondary frame or into edge channels at the canopy perimeter. Lighting cutouts, access panels, speaker openings, or sprinkler penetrations break the soffit field into modules that still need to read as one plane. Water management around canopy edges may force drip returns or sealed joints that column wraps do not require. Flatness and panel module width matter more on a soffit than on a narrow column face because large underside fields show oil-canning and joint wander more readily under lobby lighting.
Shared entrance planning starts with one cassette vocabulary: return depth, corner treatment, joint width, and panel module logic that can be repeated from column to soffit where the design allows. Where the column needs a deeper return than the soffit, that difference should be deliberate and drawn, not discovered when two shops submit unrelated details. Cassette geometry must also leave room for thermal movement and for the fixing system selected by the project team. Fabricators reading both packages together can nest sheets more efficiently and keep fold tooling settings consistent. Buyers reviewing entrance cladding should ask for column and soffit cassette sketches in the same drawing set before sheets are cut.
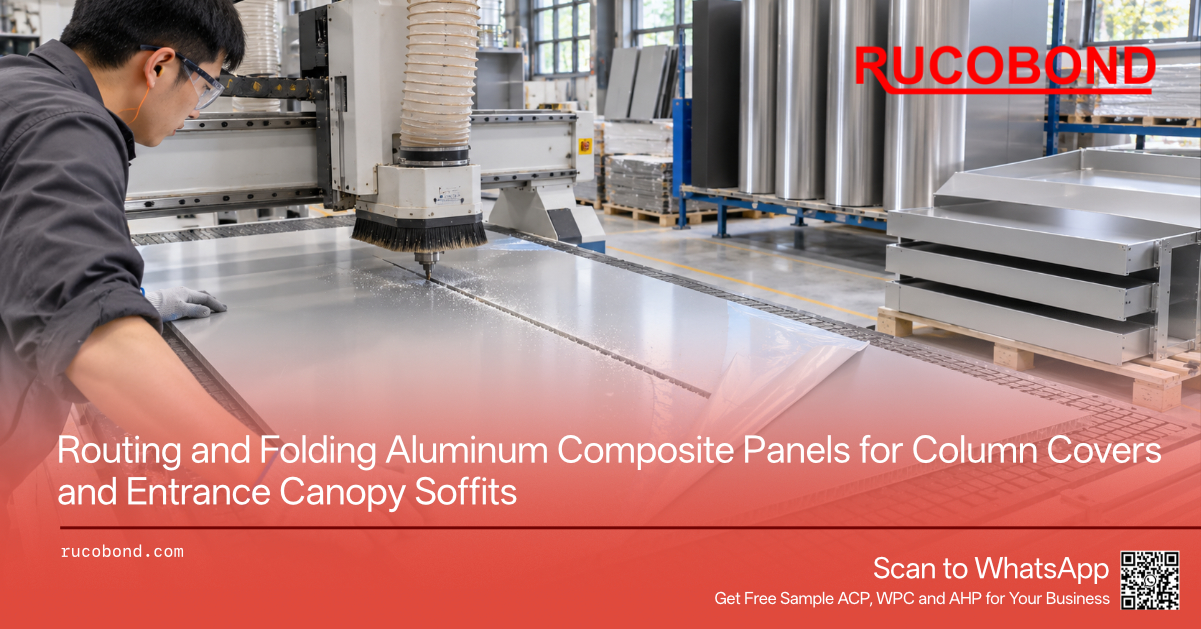
Routing and folding is the fabrication step that turns flat Aluminum Composite Panel into a cassette with returns. From the reverse face, a router or CNC removes the rear aluminum skin and part of the core along the fold line, leaving the front aluminum skin and a controlled amount of remaining core to act as the hinge. Groove geometry—tool profile, cut depth relative to the chosen panel build, and remaining core—must be set by the fabricator against the specific ACP construction and shop practice. A single “standard” groove depth is not assumed here; unverified uniform depths should not be copied across projects without confirmation against the panel build and fabrication trial results.
The panel is then folded along that groove to form a return of a planned depth. Corner quality depends on groove consistency, tool geometry, fold sequence, and the corner closure method selected for the cassette. Common shop approaches include mechanical fasteners, structural adhesives suited to the materials, or separate corner pieces detailed in the drawings. Direct welding of the ACP sandwich itself is not treated here as a general-purpose corner method; any welded detail belongs only where the project and fabricator expressly define a compatible process for that construction. Returns that are too shallow may not engage the subframe securely; returns that are too deep waste material and can leave the visible face short of the design module.
Groove consistency across a column set matters because every face of a wrap sits next to another face. Uneven grooves produce uneven fold radii and returns that fight the subframe. Soffit trays with long fold lines need the same discipline: a wandering groove shows as a wavy edge after fold. Protective film should stay on during routing and folding when shop practice allows, so the coated face is not scratched while sheets move across tables. Orientation of brushed or metallic finishes must be marked before routing so folded faces keep a continuous grain direction around a column or across a soffit run. Sharp internal corners, reverse folds, and multi-step returns raise scrap risk; complex three-dimensional returns around canopy beams often exceed clean single-groove practice and should be reviewed before nesting. Rucobond supplies ACP sheets for such programs; fabricators set routing and folding parameters to match the cassette detail, total thickness, and aluminum skin gauge on the order.
Total panel thickness and aluminum skin gauge are related but not interchangeable. A common exterior ACP sandwich may be specified by overall thickness, yet the front and rear aluminum skins can vary within the product family. Fold quality is not predicted by skin gauge alone. It emerges from the interaction of skin gauge, core type and thickness, groove geometry, remaining core at the hinge, fold radius, and processing conditions such as tool condition, fold speed, and temperature in the shop. A heavier skin can still fold poorly if the groove leaves too little or too much core, or if tooling does not match the sandwich. A lighter skin can fold cleanly when groove and process are controlled—yet it may show handling marks sooner on column faces near doors and luggage paths.
For column covers, impact and handling near entrances often push buyers to confirm skin gauge and core description together. For canopy soffits, flatness over larger modules and consistent return engagement with the frame may dominate. Choosing a thicker total sandwich without confirming skin gauge and core can still leave fold behavior unpredictable. Conversely, a heavier skin on a thin overall sandwich can change weight and handling without solving a deep-return problem that the groove-and-core relationship cannot support. Fire-performance requirements and core specification stated in the project documents must be checked at the same time as thickness and skin gauge, so the selected ACP build matches the applicable project specification rather than a color-and-thickness shorthand.
Tradeoffs should be stated in shop-drawing language: intended return depth, corner method, panel module size, face flatness expectations under lobby lighting, and any fabrication trial required before full nesting. Those fields guide which ACP build is workable. Substituting a different skin gauge or core mid-project under the same color name can change fold behavior even when total thickness matches. Entrance programs that freeze thickness, skin gauge, core description, coating, fire-performance requirement as specified, and fold return together give fabricators a stable setting for the column-and-soffit set. Product options for Aluminum Composite Panel builds are summarized on https://www.rucobond.com/Aluminum-Composite-Panel.html for buyers comparing sheet constructions before detailing returns.
Folded ACP is efficient for many column wraps and soffit trays, but it has practical limits. Deep returns, tight multi-plane corners, long unsupported spans, and profiles that need stiffening ribs or complex edge machining often favor solid Aluminum Veneer. Veneer is a single-skin aluminum panel that can be brake-formed or otherwise fabricated into shapes that exceed what a routed hinge on a composite sheet can cleanly deliver. Where the entrance design calls for pronounced three-dimensional modeling around a canopy beam, or where column covers must integrate hardware cutouts with precise edge returns, veneer may be the clearer fabrication path.
The choice is not a hierarchy of quality; it is a match between geometry, fixing-system compatibility, and product build. ACP remains suitable where flat or lightly folded cassettes, consistent coated faces, and efficient nesting across similar modules are the priority. Veneer becomes attractive when fold depth, stiffness, or edge detailing push the composite hinge beyond reliable shop practice confirmed by fabrication trials. Mixing ACP columns with veneer soffits—or the reverse—is possible when drawings declare the split and coating references are coordinated so the entrance still reads as one family. Leaving the split unspoken creates color and gloss mismatches that look like supplier error when the real issue was product-type mixing.
Buyers should compare the cassette detail against fold capability and the project’s fire-performance and core requirements before locking the material schedule. If returns on the drawing exceed practical ACP fold practice for the chosen thickness, skin gauge, and core, rewriting the detail or moving that zone to Aluminum Veneer is cleaner than forcing over-routed composite sheets. Rucobond also supplies Aluminum Veneer as an architectural panel product; the overview is at https://www.rucobond.com/Aluminum-veneer.html. Fabricators and installers still own process and fixing decisions for whichever product the drawings select. Entrance packages that state which zones are ACP-folded and which are veneer-formed receive clearer quotes and fewer mid-install material debates.
Column faces and canopy undersides share an entrance, yet they do not age under identical exposure. Column faces near the building perimeter often take rain, sun, and cleaning traffic. Canopy soffits sit more sheltered from direct weather but still collect airborne dust, traffic film, and residues from HVAC discharge or nearby cleaning; soiling builds on horizontal and near-horizontal undersides and requires planned cleaning access. Coating family selection should follow the project specification and the real exposure of each zone. Exterior architectural ACP commonly discusses fluorocarbon systems such as PVDF where outdoor weather performance is required, and polyester systems where interior or lower-exposure conditions apply. The correct assignment belongs in the project documents rather than in a late shop substitution that keeps thickness while changing the coating path.
Finish category affects how the entrance reads. Solid colors are usually more forgiving of viewing angle. Metallic and brushed finishes need orientation control around column perimeters and across soffit modules, because reversed sheets create false tone shifts at joints. Gloss targets should be written as numbers or ranges when visual continuity matters; a higher-gloss soffit beside a lower-gloss column can look like different materials under lobby light. Wood-grain or stone-inspired finishes used at entrances should be checked for repeat pattern and panel orientation so the canopy underside does not tile awkwardly against the column wrap.
Protective film type and peel timing also belong in the entrance plan. Film left too long on a sun-exposed column face can complicate inspection; film peeled early during dusty temporary works can leave the coated face vulnerable before handover cleaning. Color references for columns and soffits should come from the same approval set when the design intends a continuous skin. Rucobond offers ACP finishes across solid, metallic, brushed, mirror, wood-grain, and stone-inspired families with PE or PVDF coating options described for project discussion. Entrance purchase enquiries that attach approved finish references for both zones—together with coating family and project specification notes—reduce accidental cross-grade substitutions.
Entrance cladding fails on site as often from packing chaos as from wrong sheet builds. Column wraps and soffit trays follow different install grids; crates of anonymous mixed sheets force re-identification and wrong-bay installs. Nesting drawings should group column faces, corner pieces, and soffit modules so each pack maps to a work zone. Exterior pack labels—zone, elevation, panel mark, finish orientation—matter as much as the nest diagram inside the crate. Pack codes and batch marks also keep leftover stock from another job out of a continuous entrance field.
Protective packaging for folded cassettes differs from flat-sheet packs: returns crush without spacers or corner guards, and moisture barriers should match staging under the canopy or in a holding area. When sheets ship flat for local folding, mark column versus soffit allocations before the router queue so orientation and coating lots stay aligned. Nest for install order as well as sheet yield; a crate list that mirrors the construction sequence reduces site sorting. Detailed install choreography remains the installer’s responsibility; the material package only needs clear marks and a pack order the site can follow.
The hardest visual line on many entrances is where the column cover meets the canopy soffit edge. That junction carries changes in plane, possible sealant joints, drip details, and sometimes lighting or signage interfaces. If the column cassette return and the soffit tray edge were detailed by separate teams, the joint width, reveal depth, and finish continuity often disagree. The result is a dark gap, an overbuilt trim, or a sealant joint that reads as a repair. Joint logic should be drawn as a single detail: who owns the corner piece, which panel turns the edge, how water or dirt is managed at the transition, and how thermal movement is accommodated without forcing panels into a locked corner.
Panel module rhythm also meets at that corner. A column face width that does not relate to the soffit module grid forces awkward cut pieces at the intersection. Aligning module logic early reduces those leftovers. Metallic or brushed ACP needs a shared orientation rule across the junction so the grain does not reverse at the most viewed corner of the building. Fastener and clip visibility should be resolved in the detail against the selected fixing system; exposed fasteners on the soffit edge next to a clean column reveal look unfinished even when structurally sound.
Sealant color and joint width are part of the cladding skin, not afterthoughts. A sealant that is too dark or too glossy next to a matte ACP field pulls the eye to the joint. Entrance mock-ups or fabrication trials that include at least one column-to-soffit intersection catch these problems before full production. Where Aluminum Veneer is used on one side of the junction and ACP on the other, the detail must address different edge thicknesses and fabrication tolerances. Coordinated joint logic is a drawing problem first; material quality cannot hide a mismatched intersection.
Quotes for entrance column and soffit packages diverge when the enquiry only says “ACP for canopy and columns.” Comparable RFQs need a short, complete field set: total panel thickness; front and rear aluminum skin gauge; core specification as required by the project documents; fire-performance requirements stated in the applicable project specification; coating family; finish category and color reference; gloss target if critical; intended fold return depth; corner method; panel marks for columns versus soffits; sheet size preferences; and whether solid Aluminum Veneer is allowed or required for deep returns. Attaching simple cassette sketches with return dimensions prevents fabricators from assuming different standard returns. Do not substitute informal fire labels for the project’s written requirements; confirm the specified performance and core description against those documents without inventing rating numbers in the enquiry.
Quantity logic should separate column wrap area from soffit area and list corner pieces and access panels explicitly. Contingency quantity for damaged returns and site cuts belongs in the same list. Orientation rules for metallic or brushed finishes should appear on the drawings. Note whether sheets ship flat for local routing and folding or as finished cassettes, because pack and film needs differ. Ask whether a fabrication trial panel is required before full nesting when return depth or finish orientation is critical. Fixing-system compatibility and thermal-movement allowances should be confirmed by the design and installation teams against the cassette detail; those items belong in the drawing package even though Rucobond’s role is panel supply rather than system design or installation.
Commercial terms and product identity should stay separable. A lower unit price that changes skin gauge, core, coating family, or fire-performance path is not the same product as the approved entrance sample. Buyers comparing offers can paste the field set into every RFQ and require confirmation line by line. Rucobond supplies architectural panels to contractors, fabricators, importers, and distributors; entrance purchase enquiries that include drawings, skin gauge, core specification, fold return, coating references, and the project’s stated fire-performance requirements produce clearer technical replies than color-and-thickness shorthand. Product browsing can start from https://www.rucobond.com/ and https://www.rucobond.com/Aluminum-Composite-Panel.html when teams are still aligning terminology.
A workable entrance cladding path starts with survey and geometry, not with a color chip. Confirm column sizes, canopy underside extents, lighting and access openings, and the joint where columns meet the soffit. Decide which zones are folded ACP cassettes and which, if any, need solid Aluminum Veneer. Freeze the ACP identity: thickness, skin gauge, core specification, coating family, finish, gloss target, fold return, and fire-performance requirements as written in the project specification. Approve samples under lighting similar to the lobby approach; run a fabrication trial or small junction mock-up when schedule allows. Confirm fixing-system compatibility and thermal-movement details with the design and installation teams before full production.
Rucobond supplies Aluminum Composite Panels, Aluminum Veneer, Aluminum Honeycomb Panels, and Aluminum Coils as architectural panel products for programs that include entrance cladding. Fabricators handle routing, folding, and cassette work; installers handle site fixing and installation. Teams preparing column cover and canopy soffit packages can submit a purchase enquiry through https://www.rucobond.com/ with drawings, skin gauge, core specification, fold return depth, coating family, finish references, and the project’s stated performance requirements attached. A complete package lets the panel supplier and the fabricator work from the same picture of how the skin must wrap the columns and close the canopy underside.
Q: Can the same Aluminum Composite Panel product be used for both column covers and canopy soffits? A: Often yes, when the cassette returns, joint logic, and exposure requirements are compatible. Many entrance programs keep one ACP identity across both zones so color and gloss stay aligned. Deep or highly complex returns may still push selected pieces toward solid Aluminum Veneer while the main field remains ACP.
Q: What fold-return information should appear on fabrication drawings? A: Return depth, corner method, panel module sizes, and the engagement with the subframe should be drawn for columns and soffits. Orientation rules for metallic or brushed finishes and the column-to-soffit junction detail should sit in the same package so routing and folding settings stay consistent.
Q: When should solid Aluminum Veneer replace folded ACP at an entrance? A: When return depth, multi-plane corners, stiffness needs, or edge machining exceed clean V-groove folding on the chosen ACP build. Veneer is a different product path, not a last-minute thickness swap. Drawings should declare which zones use which product before nesting begins.
Q: How should PE and PVDF coating choices be handled on entrance cladding? A: Follow the project specification and the exposure of each zone. Column faces and canopy undersides can differ in weather and cleaning loads. Keep coating family and gloss targets consistent with the approved sample set when the design intends one continuous entrance skin.
Q: What should an entrance ACP enquiry include beyond color and thickness? A: Total thickness, aluminum skin gauge, core specification, fire-performance requirements as stated in the project documents, coating family, finish reference, intended fold return, corner method, quantities split by column and soffit, orientation rules, and simple cassette sketches. Note whether a fabrication trial is expected before full nesting.
Name: Gina Chen
Mobile:+86-189-2412-4951
Tel:+86-189-2412-4951
Whatsapp:8618924124951
Email:gina@rucobond.com
Add:Room 708, No. 8 Jingang Avenue, Nansha Street, Nansha District, Guangzhou


